Description
Note: Many products are not yet listed. Please contact us for more product information. Our supply channels are constantly expanding, and we currently have 20 stable shared supply channels. Please confirm the model, product, price, and all other necessary information with customer service before placing an order. We offer new, refurbished, and used products, and prices are adjusted according to the year of the item you require.
Key Technical Specifications
| Parameter | Value |
|---|---|
| Manufacturer | GE Fanuc |
| Model Number | IC693APU302 |
| Product Family | Series 90-30 |
| Product Series | Motion Mate APM300 |
| Product Type | Axis Positioning Module |
| Number of Axes | 2 |
| Operating Modes | Standard Mode / Follower Mode |
| Servo Loop Update | 2 ms |
| Backplane Voltage | 5 VDC |
| Backplane Current Consumption | 800 mA |
| Axis Connectors | 2 × 24-pin high-density connectors (A/B) |
| Communication Interface | Dedicated module communication port |
| Module Width | Single-slot |
| Supported CPUs | Series 90-30 CPU 311, 313, 323, 331 and higher, subject to configuration |
| Maximum Modules | Up to 3 with embedded CPUs; up to 8 with modular CPUs 331 and higher |
| Maximum Modules per Baseplate | 3 |
| Stored Motion Programs | Up to 10 |
| Firmware | Hardware-dependent revisions; firmware version 2.80 documented for later revisions |
Technical reference: GE Fanuc Motion Mate APM documentation, GFK-1317G, and Series 90-30 installation documentation. Actual capabilities depend on hardware revision, firmware, CPU firmware, and programming software compatibility.
Manualzz+2
Product Introduction
The GE Fanuc IC693APU302 is a programmable two-axis Motion Mate APM300 positioning module designed for Series 90-30 PLC systems. It provides coordinated motion control functions, allowing a PLC to manage two motion axes within an integrated automation architecture.
The module supports Standard and Follower operating modes. Its 2 ms servo loop update makes it suitable for applications requiring frequent motion-control updates, while Follower Mode supports electronic gearing between master and slave axes. Up to 10 motion programs can be stored in the module.
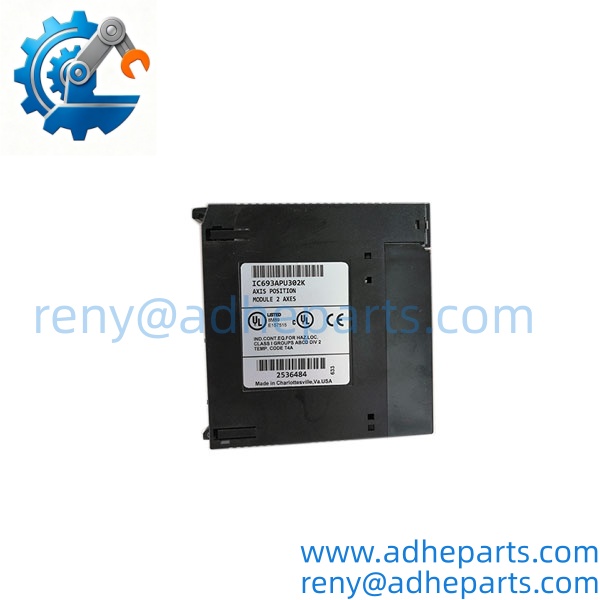
IC693APU302
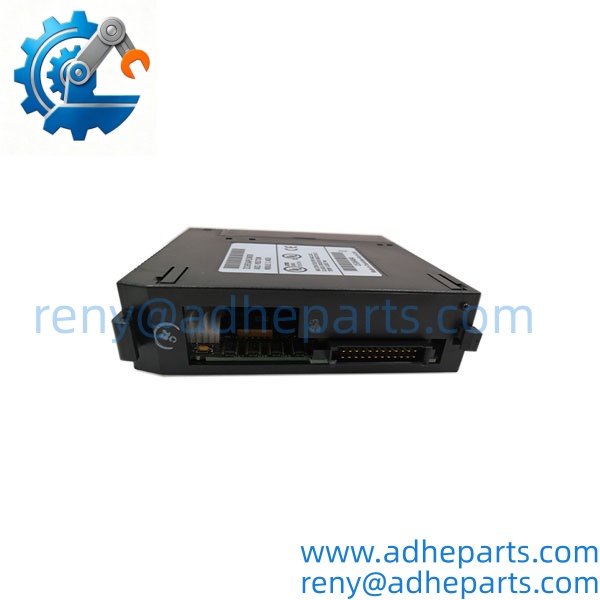
IC693APU302
IC693APU302
IC693APU302
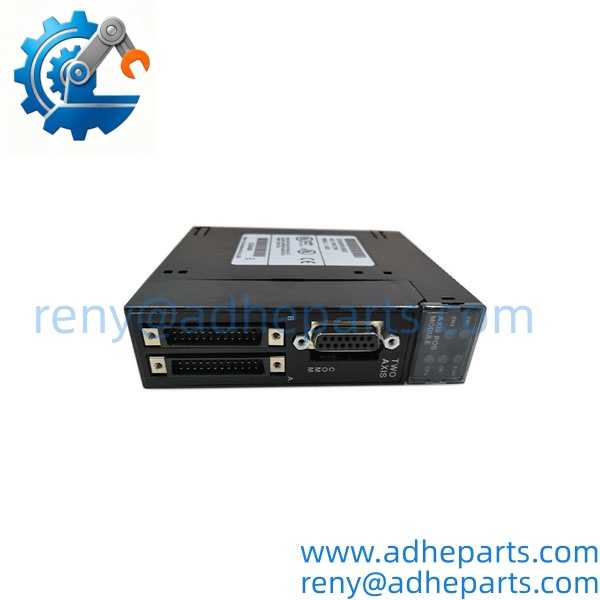
IC693APU302
Application Scenarios & Field Experience
Part 1 – Engineering Challenges
In automated production machinery, replacing a failed motion controller can be more complicated than replacing a standard PLC I/O module. Axis positioning, servo response, master-slave synchronization, and existing motion programs must all remain compatible with the machine’s original control architecture.
The IC693APU302 addresses these requirements by integrating two-axis motion control with the Series 90-30 PLC. Its Follower Mode is particularly useful in applications where a slave axis must maintain a defined relationship with a master axis. This is important in continuous-feed machinery, where synchronization errors can affect product positioning and machine throughput.
Part 2 – Typical Application Scenarios
1. Packaging Industry – High-Speed Packaging Machinery
- Process: Film feeding, cutting, and synchronized packaging operations.
- Requirement: Two-axis positioning and electronic gearing to maintain synchronization between feeding and cutting mechanisms.
2. Printing Industry – Industrial Printing Equipment
- Process: Web handling, roller synchronization, and material positioning.
- Requirement: Follower Mode for maintaining coordinated movement between master and slave axes.
3. Automotive Manufacturing – Automated Assembly Lines
- Process: Servo-driven positioning tables and material transfer mechanisms.
- Requirement: Independent control of two motion axes within an existing PLC architecture.
4. Material Handling – Conveyor and Transfer Systems
- Process: Synchronized conveyor drives and automated transfer equipment.
- Requirement: Programmable positioning and coordinated axis movement for repeatable material handling.
Part 3 – Illustrative Field Case
A packaging plant experienced an unexpected motion-control failure that affected synchronization between its film-feeding and cutting mechanisms. The maintenance team traced the fault to the existing two-axis positioning module. A compatible IC693APU302 replacement was sourced, and engineers checked the hardware revision, firmware, CPU compatibility, and stored motion configuration before commissioning. After restoring the original operating parameters and verifying both axes, the machine returned to production.
Illustrative engineering scenario, not a documented customer installation.
Standard Operating Procedure (SOP) for Quality Control
Our QC process for the GE IC693APU302 focuses on hardware identification, electronic condition, connector integrity, and motion-control functionality.
1. Visual & Origin Inspection
- Verify the GE Fanuc identification label and IC693APU302 model number.
- Inspect the PCB, electronic components, and module housing.
- Check the two 24-pin high-density axis connectors for bent pins or physical damage.
- Inspect available OEM labels, packaging, and identification markings.
- Check for corrosion, burned components, previous repairs, or unauthorized modifications.
- Record the actual hardware revision and product condition.
2. Live Rig Testing
- Verify the Series 90-30 rack and 5 VDC backplane power requirements.
- Check module power-up behavior and diagnostic indicators.
- Inspect EN1, EN2, STAT, OK, and CFG status indicators.
- Where a compatible test setup is available, verify module communication and axis interface operation.
- Check Standard and Follower Mode functionality under an appropriate test configuration.
- Verify servo command and feedback behavior using compatible test equipment.
3. Firmware Verification
- Record the module’s hardware revision and firmware version.
- Check compatibility with the installed Series 90-30 CPU firmware.
- Verify programming software requirements.
- Confirm that motion program configurations are compatible with the replacement module.
- Document firmware differences before shipment.
4. ESD-Safe Packaging
- Handle the module using ESD-protected procedures.
- Place the module in anti-static packaging.
- Protect the high-density connectors against impact and contamination.
- Add suitable cushioning for international transportation.
- Verify the model number and shipping information before dispatch.
5. Pre-Shipment Documentation
- Provide actual product photographs upon request.
- Arrange live video inspection before shipment.
- Confirm model number, hardware revision, condition, and quantity.
- Provide tracking information after dispatch.
Frequently Asked Questions (FAQ)
Q1: Is the GE compatible with all Series 90-30 PLC CPUs?
A: The is designed for the GE Fanuc Series 90-30 PLC platform. It supports embedded CPUs 311, 313, and 323, as well as modular CPUs 331 and higher, subject to system configuration and firmware requirements.
However, it should not be assumed compatible with every GE PLC platform. For example, the is not listed as supported in the PACSystems RX3i universal backplane architecture. Always verify the CPU model, baseplate, firmware, and programming software before ordering.
Q2: What warranty do you provide for the ?
A: We offer a 12-month warranty, subject to confirmed order terms. The warranty covers qualifying product-related failures under normal operating conditions. Physical damage, incorrect installation, and unauthorized modifications are excluded.
Q3: Is the GE still available, and how quickly can it ship?
A: The is a discontinued product, so availability generally depends on surplus inventory and refurbished stock. We can check actual stock condition, provide product photographs, and arrange live video inspection before shipment.
For confirmed available inventory, our standard shipping arrangement is generally within one week after payment.
Q4: Can firmware differences affect replacement compatibility?
A: Yes. Hardware and firmware revisions matter.
For example, the documented firmware version 2.80 requires Series 90-30 CPU firmware version 3.52 or higher and compatible programming software version 6.01 or higher.
Before replacement, check:
- Existing APM hardware revision.
- Current firmware version.
- Host CPU firmware version.
- Programming software compatibility.
- Existing motion program configuration.
Do not assume that every revision supports identical features.
Manualzz
Q5: What should engineers check before installing the ?
A: Several points deserve attention before installation:
- Confirm the correct Series 90-30 baseplate and CPU configuration.
- Verify the 5 VDC backplane power budget; the module requires approximately 800 mA.
- Check the two 24-pin axis connectors and cable pin assignments.
- Verify servo drive compatibility and feedback wiring.
- Confirm Standard or Follower Mode configuration.
- Check motion program parameters and axis direction.
- Verify hardware and firmware revisions before commissioning.
Important: Do not remove or install the module under power unless the applicable system documentation explicitly permits hot swapping. Incorrect wiring, incompatible firmware, or incorrect motion parameters can cause unexpected axis movement, positioning errors, or machine downtime. Always follow the approved machine shutdown and commissioning procedures.